- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик



Die Casting Pump Body
Xiamen Hongyu Intelligent Technology Co., Ltd. is capable of completing the mold design, processing and delivery of pump bodies. Die Casting Pump Body, as a component for carrying fluid equipment on vehicles, has special process control measures for vibration leakage and medium corrosion risks. Relying on the complete processing equipment within the factory, customized processing can be carried out based on drawings or physical samples. You can send an email to request samples and the complete technical materials.
Send Inquiry
Product Description
Xiamen Hongyu Intelligent Technology Co., Ltd. specializes in the processing and manufacturing of fluid die-cast pump bodies. The Die Casting Pump Body is the basic load-bearing component of the pump assembly, responsible for medium diversion and component assembly positioning. We fully cover all processes from mold development to finished product inspection, and can adapt to various assembly conditions of vehicle-mounted equipment.
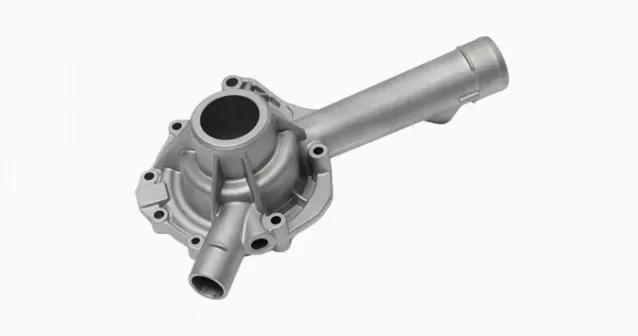
Product Basic Explanation
The Metal pump body serves as the external base of the fluid pump, with internal formed flow channels and assembly reference positions reserved, used to accommodate internal components such as impellers and seals, achieving physical isolation between the external environment and the transported medium. This component continuously withstands the internal pressure of the medium and the alternating vibration loads brought by the vehicle's operation. The size and positional accuracy of the component directly determine the overall operational stability of the pump assembly. It can be adapted to cooling fluid pumps, fuel delivery pumps, and other fluid equipment.
Product Core Performance
1.Structural Anti-Vibration Performance
During the early stage of structural design, the pump body manufacturer optimizes the transition area of the shell wall thickness to eliminate stress concentration points. The shell can pass the reliability test of continuous high-frequency vibration, and after the test, there is no cracking or medium leakage. The installation reference surface of the shell is strictly controlled for plane accuracy to ensure the coaxiality of internal components and reduce abnormal wear during long-term operation. In the face of high-vibration conditions, the shell reinforcement layout can be further strengthened by adjusting the layout of the shell ribs.
2.Forming Process Performance
Aluminum die casting can achieve integrated molding of complex internal cavities, eliminating the shell assembly welding structure. The die-casting process can reduce the probability of internal air holes in the blank, avoiding leakage risks under high-pressure bearing conditions. The die-casting blank is reserved with reasonable processing allowance, and subsequent CNC only performs fine processing on the sealing surface and installation holes, reducing the overall machining time. Complex flow channels do not need to be divided into multiple parts for assembly, effectively avoiding cumulative tolerances caused by multiple component assembly, and compared with welded shells, it can also reduce the risk of weld failure.
3.Standardized Process Inspection
The die casting manufacturer sets fixed inspection nodes for each process. After the blank is completed, the first piece full-size inspection is carried out; semi-finished products are conducted batch-based air-tightness sampling inspections; all finished products are completed with 100% pressure tests before shipment. Each batch retains the original test data with batch numbers for you to review. All detection measuring equipment is subject to regular calibration to ensure the objective and effective output of the detection results.
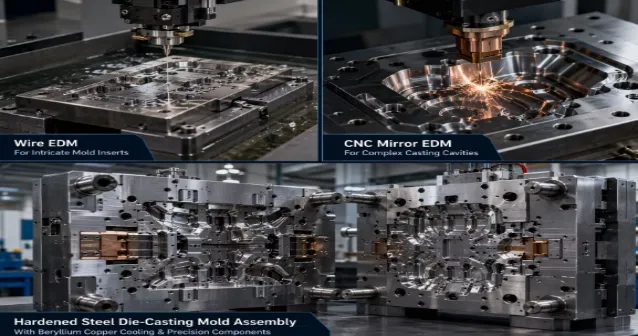
4.Operating Condition Selection Reference
The automobile pump body can adapt to the working environment with frequent temperature fluctuations during vehicle operation. The shell can be treated with passivation or spraying for anti-corrosion, meeting the requirements for outdoor corrosion resistance. The aluminum alloy substrate has a medium usage boundary. If your project involves special transportation media with strong corrosion, please inform us in advance, and we will conduct an assessment of material and surface treatment alternative solutions.
Technical Parameter List
| Project | Parameter Description |
| Product Name | Die Casting Pump Body |
| Molding Process | High-pressure die casting, CNC precision machining, surface anti-corrosion treatment |
| Optional Materials | ADC12, A380 aluminum alloy, material customization is supported |
| Applicable Temperature | -40℃ to 130℃ |
| Air Tightness Indicator | No leakage after maintaining pressure at 0.5 MPa for 40 seconds |
| Critical Tolerances | Installation surface flatness 0.03mm, hole position tolerance ±0.04mm |
| Customization Method | Design drawings, physical samples customization, sample production is supported |
Note: The above table represents general reference parameters. The actual indicators shall be based on the technical documents confirmed by both parties; ADC12 and A380 aluminum alloys are not suitable for strong corrosive media. In extreme working conditions, a special process assessment can be initiated.
Vehicle-mounted pump housing drop scenario
Die cast automotive pump housing are mainly used in vehicle cooling and fuel delivery assemblies, suitable for cooling fluid circulation pumps and low-pressure fuel pumps of passenger cars and light commercial vehicles. We have multiple batches of corresponding housing export drop projects, with complete archived drawing versions and full test reports.
Sample and Packaging Delivery
Die Casting Pump Body sample processing is protected against rust after processing. It is isolated with foam and encapsulated in a hard cardboard box to avoid damage to the precision processed surfaces during transportation. The sample has a fixed processing cycle, and the related sample costs can be confirmed through email. The sample is accompanied by material certificates and airtightness test documents; for batch orders, it will be shipped according to the logistics channel you specify, and the complete set of shipping vouchers will be simultaneously transferred.
Custom Project Cooperation Process
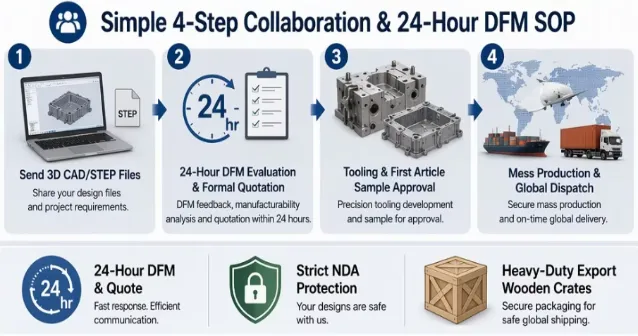
1. Requirement Collection: Receive the drawings and physical samples provided by you, confirm the working conditions, conveying medium, tolerances, and estimated order quantity information.
2. Process Assessment: Engineers complete the DFM process analysis and output the process assessment document and project quotation within 4 working days; the special assessment for extreme working conditions will have an appropriate extension of the cycle.
3. Mold Manufacturing: After scheme confirmation, start mold processing. The standard cycle is 22 days, and the progress of mold processing nodes will be updated synchronously.
4. Sample Testing and Sampling: After the mold is completed, conduct sample testing, produce T1 samples, and complete the full set of project testing.
5. Sample Delivery: Qualified samples are sent out, accompanied by complete test records, supporting re-inspection by third-party institutions.
6. Scheme Adjustment: Receive feedback from sample testing, and carry out mold repair, process parameter adjustment as needed.
7. Mass Production: After the sample is confirmed to be error-free, start mass production, and regularly synchronize the production progress.
8. Inspection and Delivery: After all detection processes of the finished products are completed, they are packaged and shipped, and the corresponding batch set of technical documents will be transferred.
Why choose us?
We have many years of practical experience in die-casting pump body processing. Our factory is equipped with die-casting units, CNC processing centers, and a complete set of physical and chemical testing equipment. Die Casting Pump Body from mold development to finished product inspection are all completed in the factory, without outsourcing subcontracting links. Leveraging the experience accumulated from similar projects in the past, we can identify potential risks at the structural and material levels in the early stage of the project, reducing the need for repeated adjustments. Each batch of products retains complete material reports and air-tightness test records, facilitating project review and traceability. The product enjoys a 12-month warranty. For issues caused by production process defects, we will bear the rework costs; damages caused by assembly errors or improper medium selection are not covered by the warranty. If you have project intentions, you can send an email. We can arrange samples for you and collaborate to promote the project implementation.
FAQ
What type of pump is this (water, oil, chemicals, automotive use)?
This die-cast housing is specifically designed for automotive oil pump applications and is not suitable for chemical liquids without additional coating solutions.
Why is die-casting chosen over sand casting in pump manufacturing?
Die-casting enables more precise size tolerances, better surface finish, and stable batch consistency, with shorter delivery cycles, making it ideal for mass production of compact automotive pump housings.
How do you prevent defects such as air holes and leakage?
We optimize the gating system, control the injection parameters, and use vacuum die-casting technology. At the same time, strict pressure tests will be conducted to eliminate the risk of leakage.
What information and file formats do you need to provide to get a quote?
Please provide 3D CAD files in STEP, STP, IGS or X_T formats, as well as 2D drawings in PDF or DWG format with specific tolerances, surface finish and material requirements. If you don't have a CAD model, detailed samples or concept sketches with key dimensions can also be accepted.
Can test reports and material certificates be provided during shipment?
Corresponding reports can be provided upon request.
How do you usually package the products?
We can provide packaging according to your requirements. Products with high appearance requirements will be individually packaged in a plastic box, and finally shipped in a cardboard box or wooden box.
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.