- English
- Español
- Português
- русский
- Français
- 日本語
- Deutsch
- tiếng Việt
- Italiano
- Nederlands
- ภาษาไทย
- Polski
- 한국어
- Svenska
- magyar
- Malay
- বাংলা ভাষার
- Dansk
- Suomi
- हिन्दी
- Pilipino
- Türkçe
- Gaeilge
- العربية
- Indonesia
- Norsk
- تمل
- český
- ελληνικά
- український
- Javanese
- فارسی
- தமிழ்
- తెలుగు
- नेपाली
- Burmese
- български
- ລາວ
- Latine
- Қазақша
- Euskal
- Azərbaycan
- Slovenský jazyk
- Македонски
- Lietuvos
- Eesti Keel
- Română
- Slovenski
- मराठी
- Srpski језик
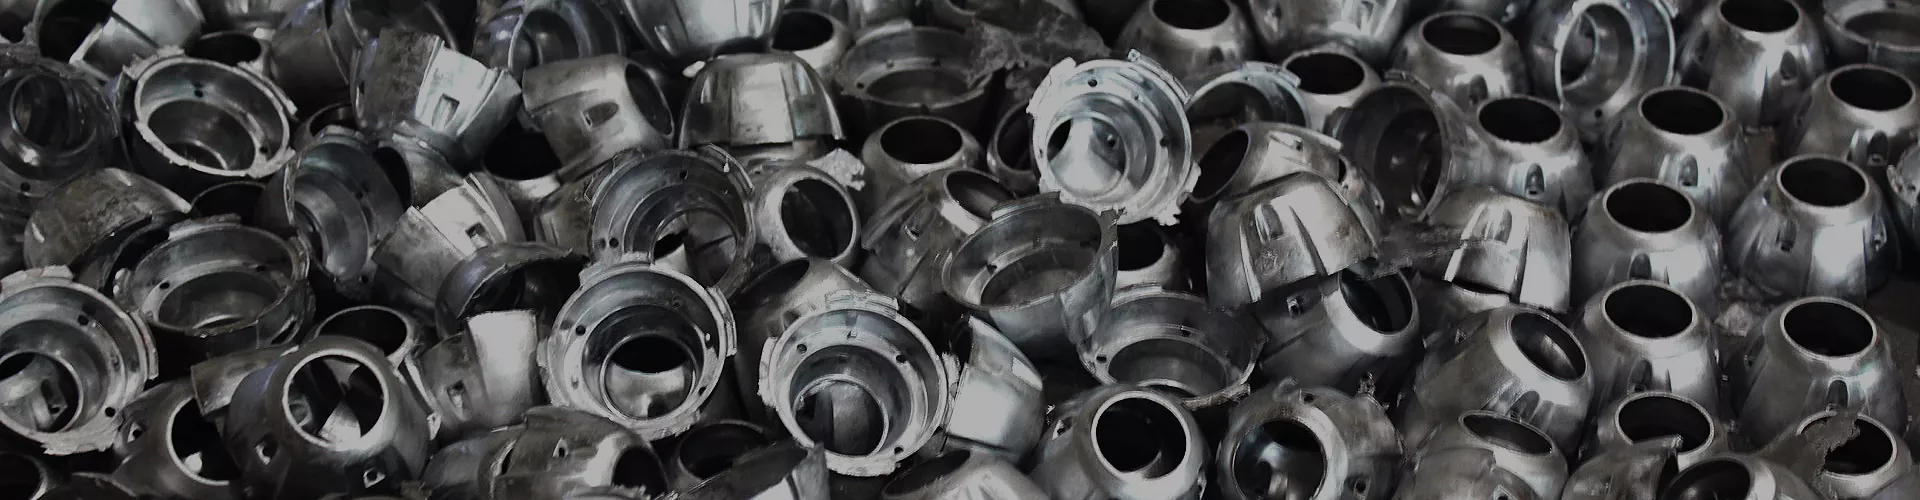



Casting Engine Components
Xiamen Hongyu Intelligent Technology Co., Ltd. specializes in the customized development of lubrication pump housing die-cast parts in the Casting Engine Components. We focus on the key components of the engine lubrication system and leverage our professional manufacturing capabilities to provide overseas power equipment customers with stable quality and controllable delivery batch supply solutions.
Send Inquiry
Product Description
Product Introduction
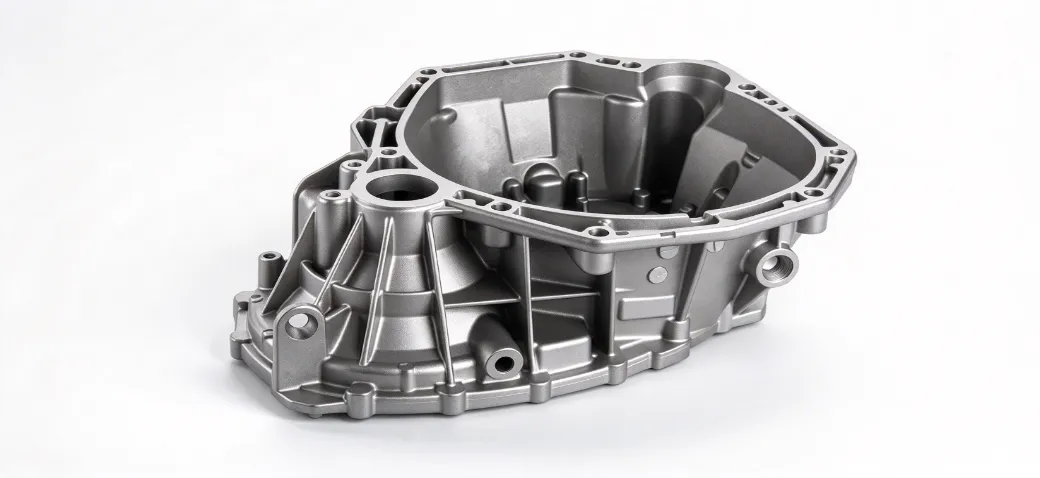
The oil pump housing is the core component of the engine lubrication system, and the accuracy of the internal flow channels and the sealing performance directly determine the reliability of the entire lubrication system. After being formed by a single-piece die-casting process and then processed by CNC precision machining, the finished product is obtained. Compared with the welding assembly method, die-casting has significant advantages in structural strength, batch cost, and dimensional consistency. In the engine parts category, the pump housing is one of the most stringent force-bearing components with the highest requirements for internal tightness.
Core Strengths
1. Pre-pressurization Simulation
The internal flow channels of the lubrication pump are complex. The traditional die-casting solution often leads to high batch leakage rates due to entrained air and porosity. Before mold development, we conducted MAGMAmasoft die-casting simulation to predict the location of entrained air and the tendency of porosity, avoiding production defects at the design stage, and reducing the number of mold modifications by 40% compared to the conventional solution.
2. Precision Machining Control
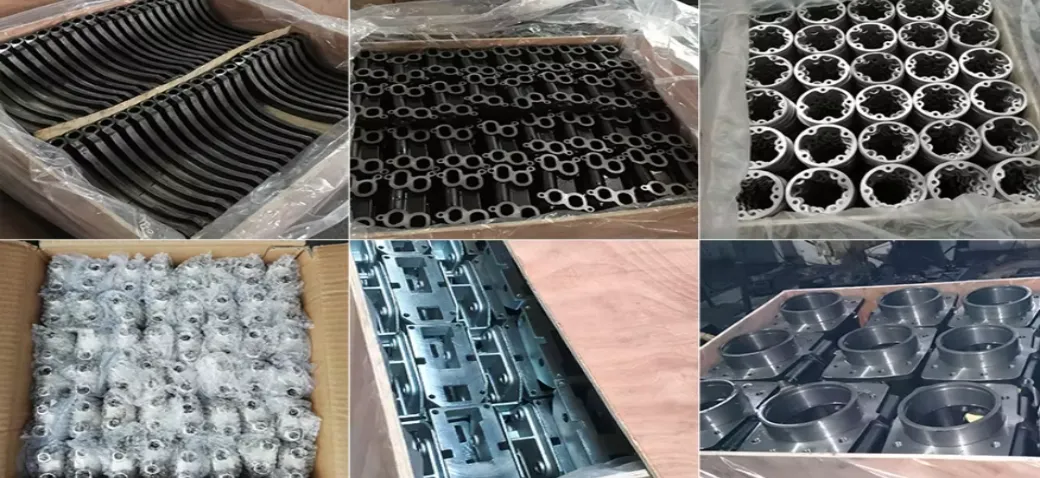
The dimensional tolerances of the internal cavity and installation surface of the pump housing directly affect the volumetric efficiency and sealing life of the pump body. We use a machining center to complete multi-face processing in one setup, and the key dimensions have a stable CPK value of above 1.33, ensuring the stable formation of thin-walled structures. Precision parts such as the crankshaft peripheral brackets can also be completed on the same production line to ensure uniform processing standards for different products.
3. Material Adaptability for Various Power Conditions
All structural schemes are evaluated for material selection and processing technology simultaneously during the design stage. The pump housing for passenger cars diesel engines is subjected to high-temperature oil impact for a long time. The aluminum alloy material has both oil resistance and casting fluidity, reducing weight by 20% compared to similar solutions. We can flexibly select materials based on your working conditions, covering long-term usage scenarios from normal temperature to 120°C.
Materials and technical specifications
| Project | Parameter Description |
| Product Name | Casting Engine Components |
| Basic Process | High-pressure die casting, CNC precision machining, heat treatment, surface passivation |
| Optional Materials | ADC12/A380 aluminum alloy, H62 copper alloy (selected as per requirement) |
| Tolerance Grade | Shaft hole position ±0.02mm, Installation surface flatness 0.03mm |
| Air Tightness Test | Pressure maintained at 0.5MPa for 30 seconds without leakage |
| Warranty Period | 12 months from shipment date. No human-induced damage issues will be charged for free replacement |
| Service Mode | ODM/OEM customization, support for small batch samples |
Note: The above are general reference specifications for the pump housing type. The final parameters shall be based on the confirmed drawings by you. For special pressure resistance and special medium working conditions, please communicate in advance and conduct preliminary process assessment.
Die Casting Process and Quality Control
For the Casting Engine Components, we have increased the frequency of regular mold maintenance. We conduct mold maintenance every 5,000 mold cycles to ensure the consistency of the pump body blanks.Maintenance is carried out every 5,000 mold cycles to ensure the consistency of the pump body blanks. Every 5,000 mold production cycles, mold maintenance is carried out to ensure the consistency of the pump body blanks. After the die casting blanks are completed, the following processes are sequentially carried out: deburring, CNC fine milling, flow channel cleaning, and surface treatment to remove the processed debris.
The cylinder head shell type with the same process platform can stably replicate the above quality standards. The first piece of each batch of blanks must be confirmed by three-coordinate measurement, and the deviation of key dimensions should be controlled within the tolerance range to allow for mass production.
The marine auxiliary pump housing is used in the high-humidity and high-salt environment at sea for a long time. We have made special upgrades to the surface treatment process. The neutral salt spray test of marine engine parts can reach more than 720 hours. During the incoming material process, the material grade is checked and the material certificate is retained. Die casting blanks are sampled and X-ray inspected by batch to check for internal defects. All inspection records are archived and saved by batch.
Application Areas and Selection Key Points
This type of pump housing is widely used in passenger car diesel engines, marine auxiliary machinery, generator sets, and other fields.The car engine parts have a high requirement for lightweighting. The aluminum alloy die casting solution can effectively reduce the overall weight of the machine and improve fuel efficiency. During the selection stage, the types of oil, working pressure, temperature range, interface specifications, and installation space need to be confirmed. In the parts engine category, the pump housing is our core focused category. We recommend that you provide complete drawings or physical samples, and our engineering team will complete the die casting feasibility assessment and output the preliminary plan.
Customized cooperation process
1. Document/Sample Reception: Receive your 2D drawings, 3D models or physical samples, and collect project information such as working conditions, materials, batch size, and tolerance requirements
2. Engineering Evaluation: Complete the die-casting feasibility analysis, risk point identification, and preliminary quotation output within 3 working days
3. Mold Development: Customize the die-casting mold. The standard cycle is 25 days. Complete trial molding, mold revision, and first-piece size verification
4. Sample Production: Produce T1 samples. Deliver within 10 working days. Complete full inspections of dimensions and air tightness
5. Batch Production: After sample confirmation, start batch production. The delivery time for the main product is 20-30 days. Implement full process quality control
6. Inspection and Delivery: Complete final inspection and packaging. Arrange for shipment according to the delivery schedule. Simultaneously deliver complete batch inspection materials
Why choose us?
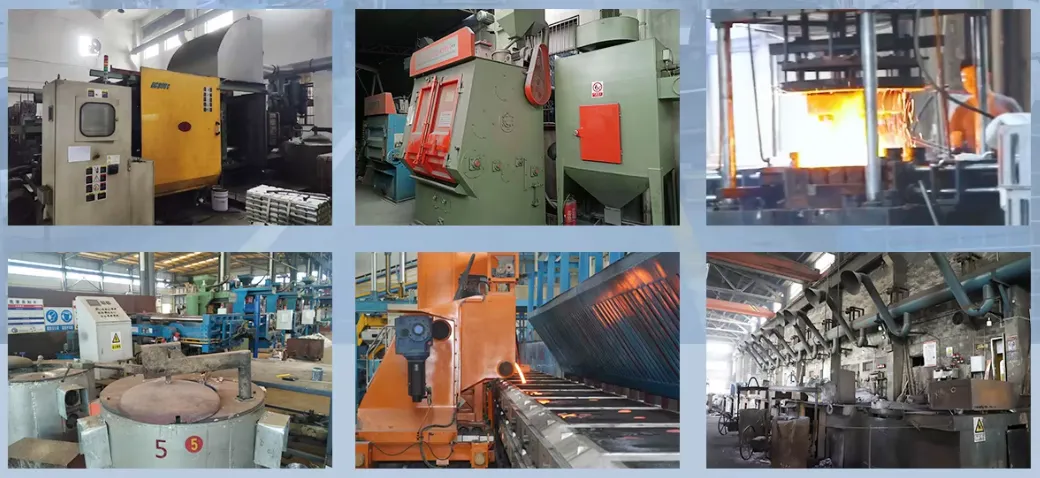
We have an independent mold processing workshop and a die-casting production workshop. We have a total of 12 800T-2000T die-casting machines, with 12 years of focus on producing pump housing type die-cast parts.As a die cast engine parts manufacturer, our products have been exported to 12 countries and regions including Germany, the United States, and Japan. We are familiar with the ISO 9001 and IATF 16949 automotive quality systems. We can provide all the quality documents such as material sheets, flaw detection reports, and inspection records according to customer requirements. We can flexibly meet the demand for different batch orders. Our core product, Casting Engine Components, achieves a balance between batch cost and operational reliability through integrated manufacturing capabilities. The sample fee can be fully deducted from the bulk order. You can send us an email at any time to obtain sample plans or technical evaluations. Our engineering team will reply within 2 working days.
FAQ
Can you customize the die-cast parts of the oil pump housing based on the drawings?
Sure. We support customized development based on 2D drawings, 3D models or physical samples.
What payment methods do you support?
Flexible payment terms can be negotiated according to the actual situation. We support various international trade settlement methods such as T/T and L/C.
How much dimensional tolerance can the product achieve?
Regularly, it can reach ±0.02mm, following the tolerance specified in the drawings.
Can test reports be provided for mass-produced products?
We can provide material certificates and batch inspection records according to your needs.
Do you support engraving logos and part numbers on the products?
We support mold engraving or laser marking.
Related Category
Send Inquiry
Please feel free to give your inquiry in the form below. We will reply you in 24 hours.